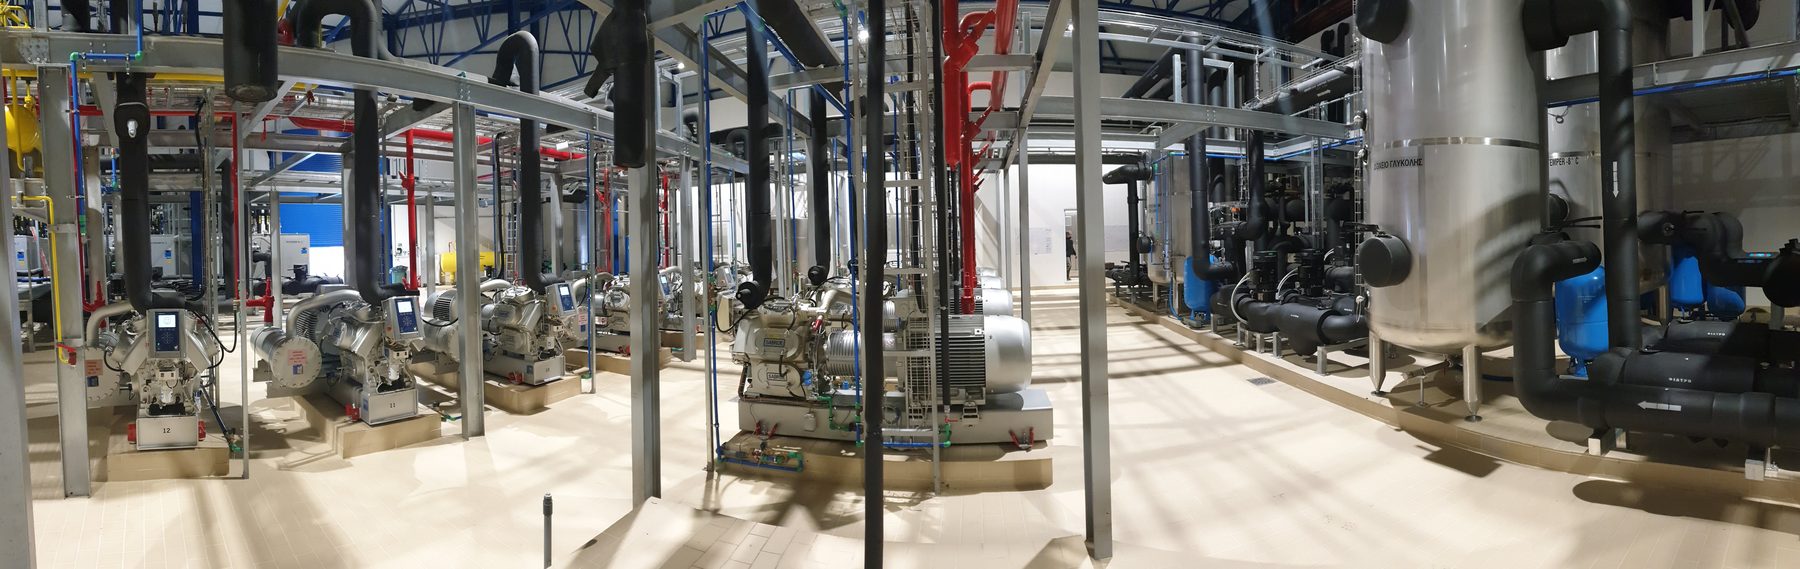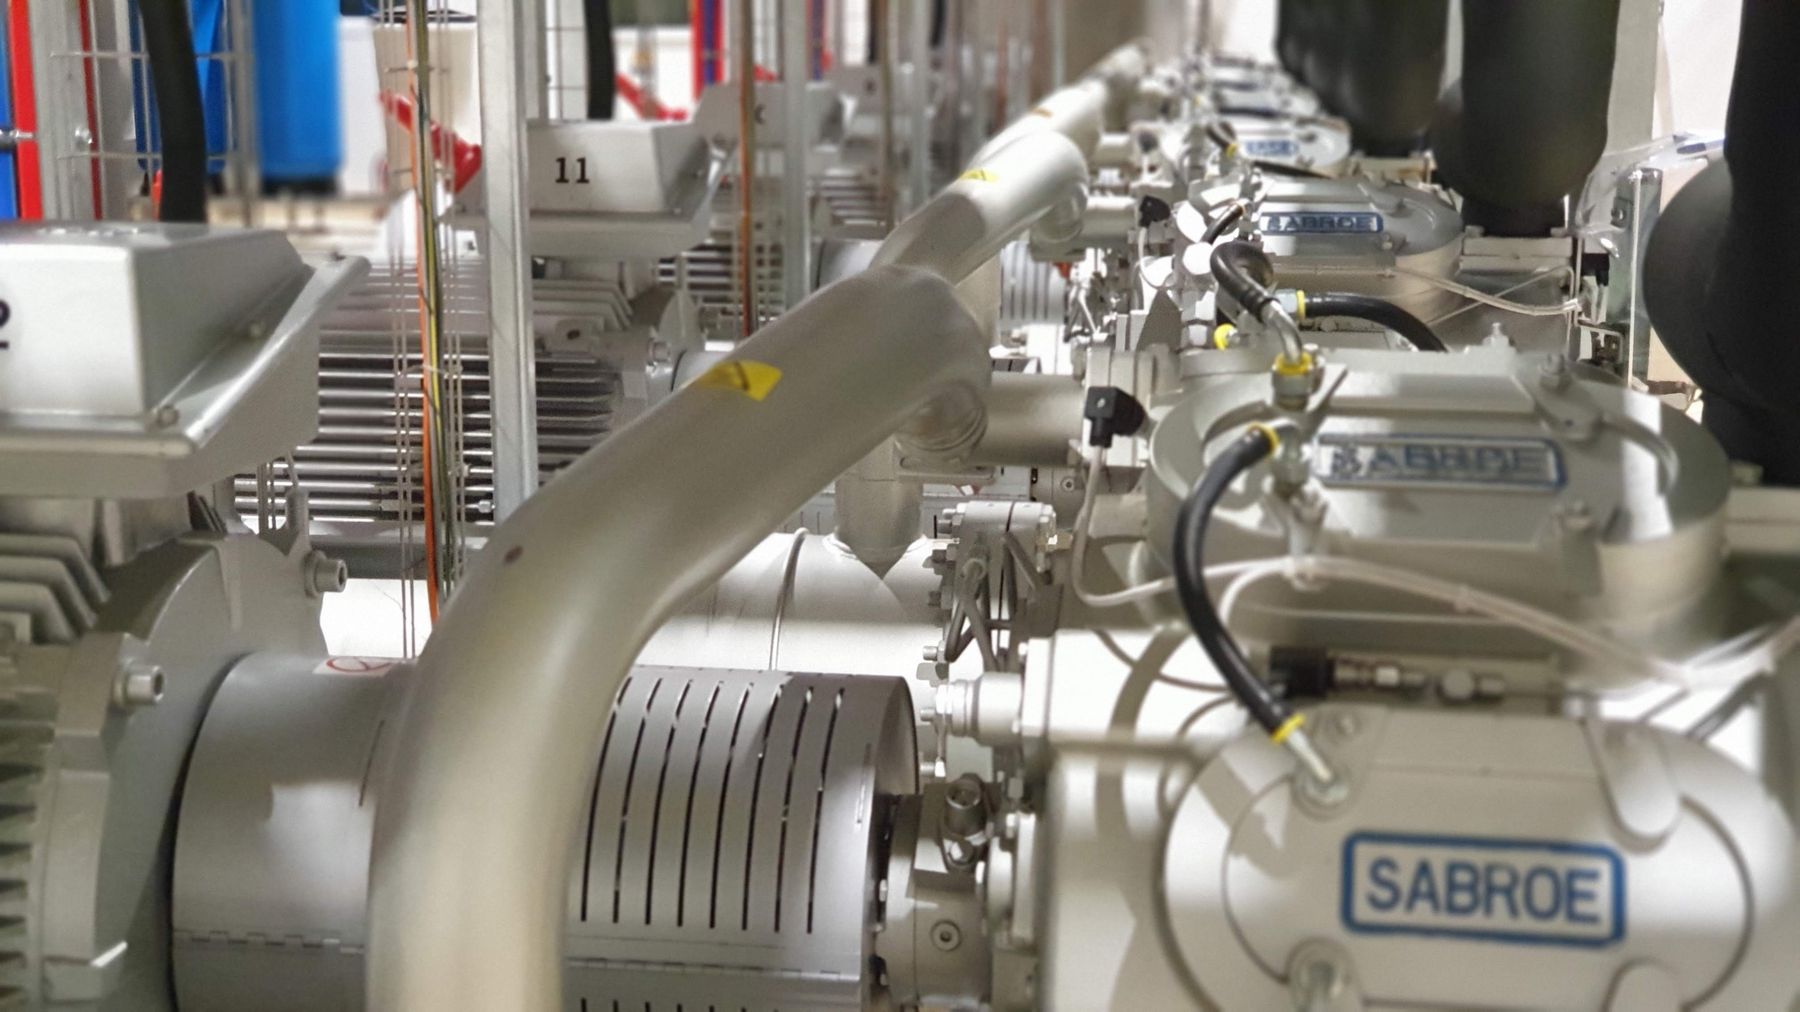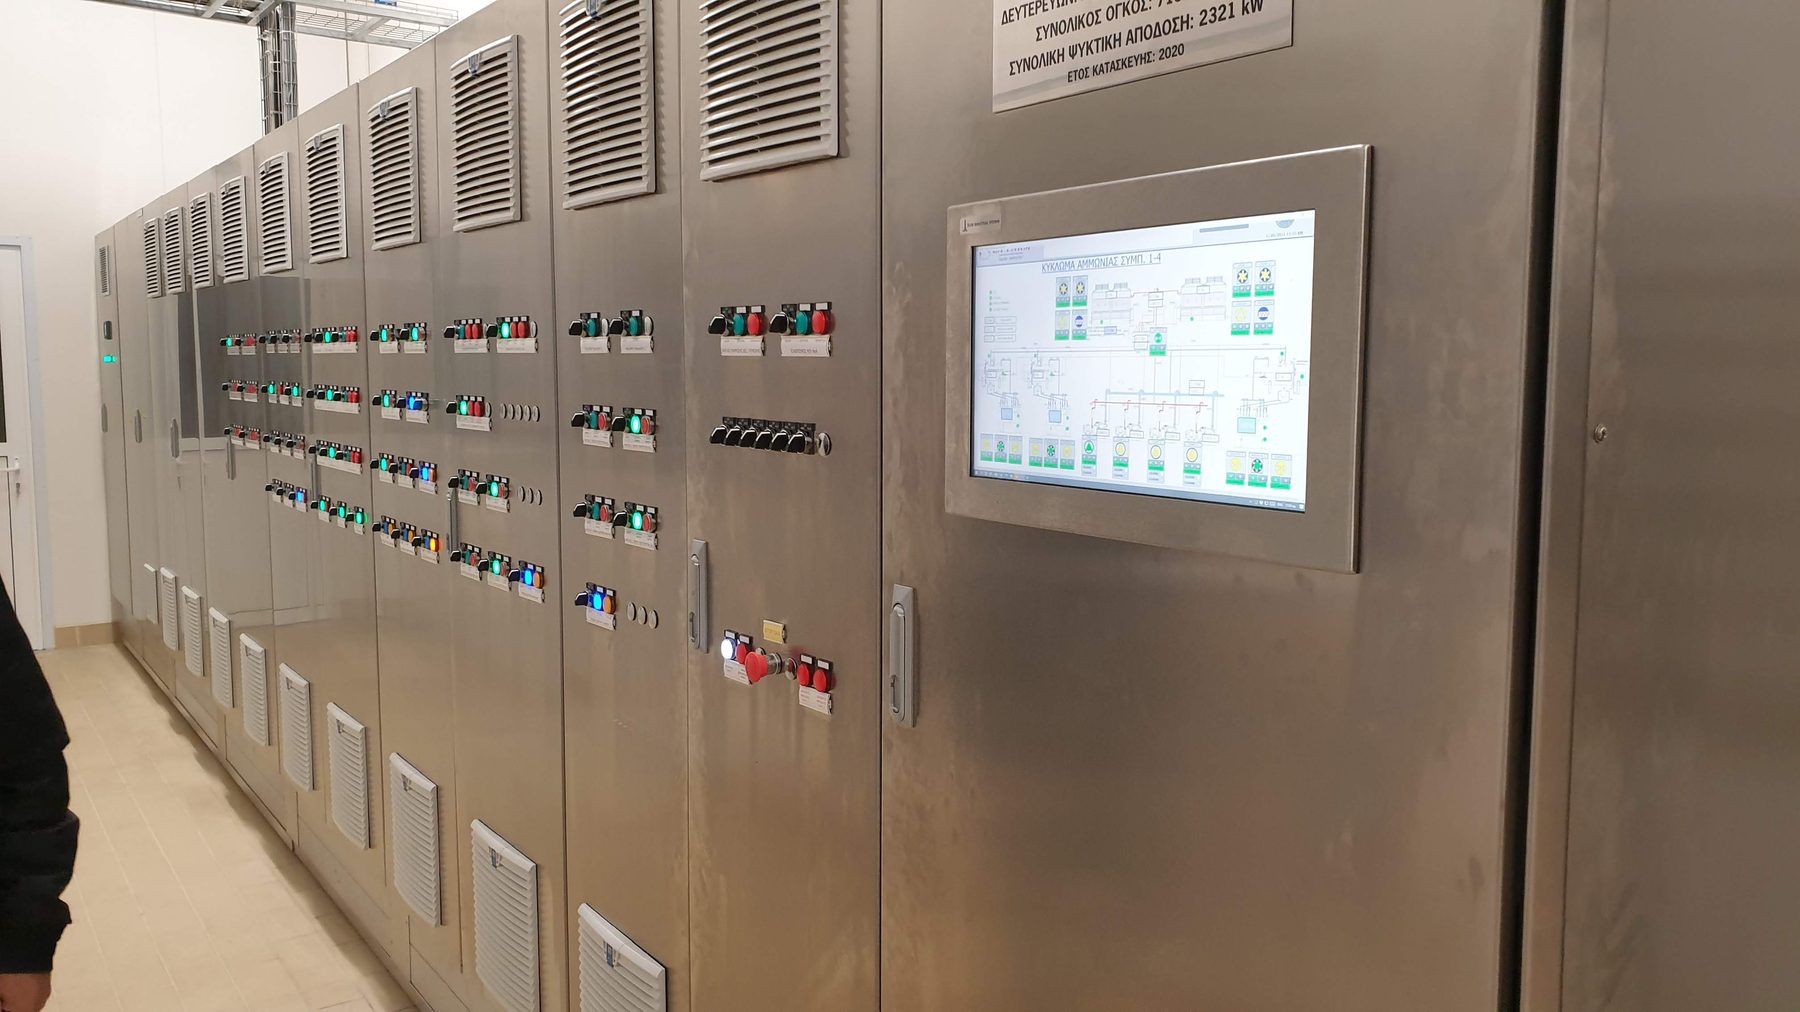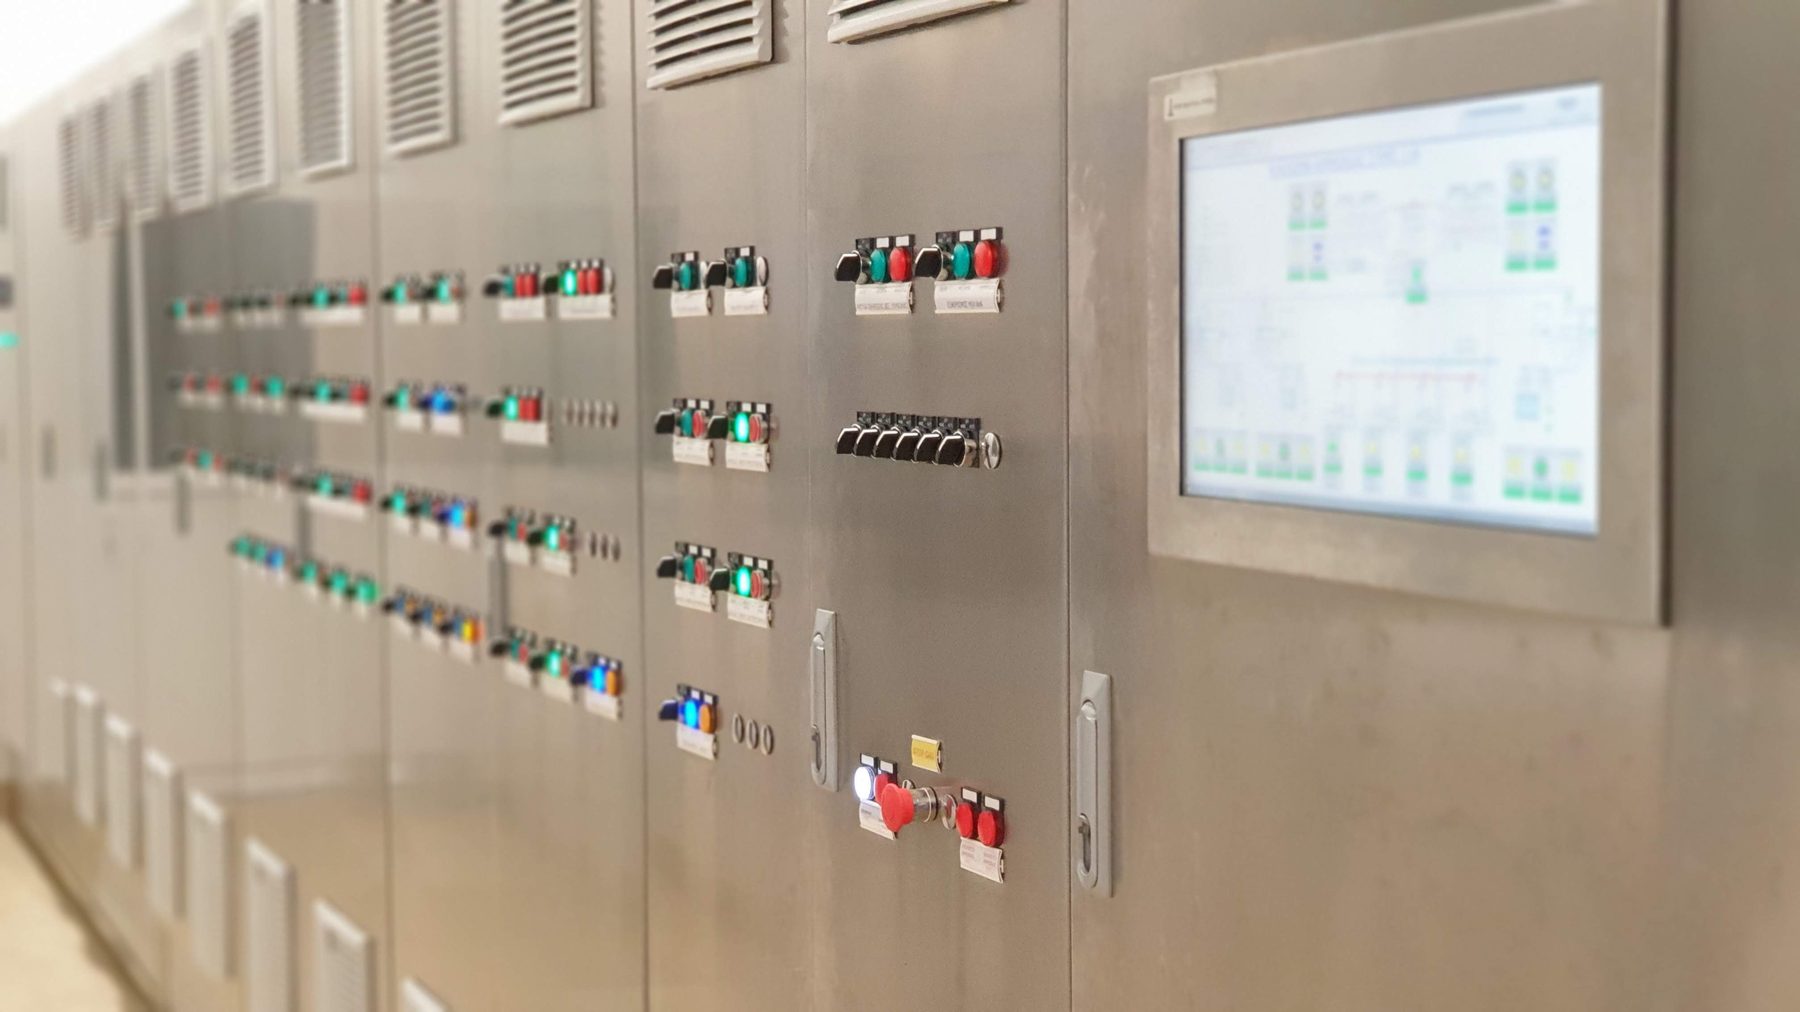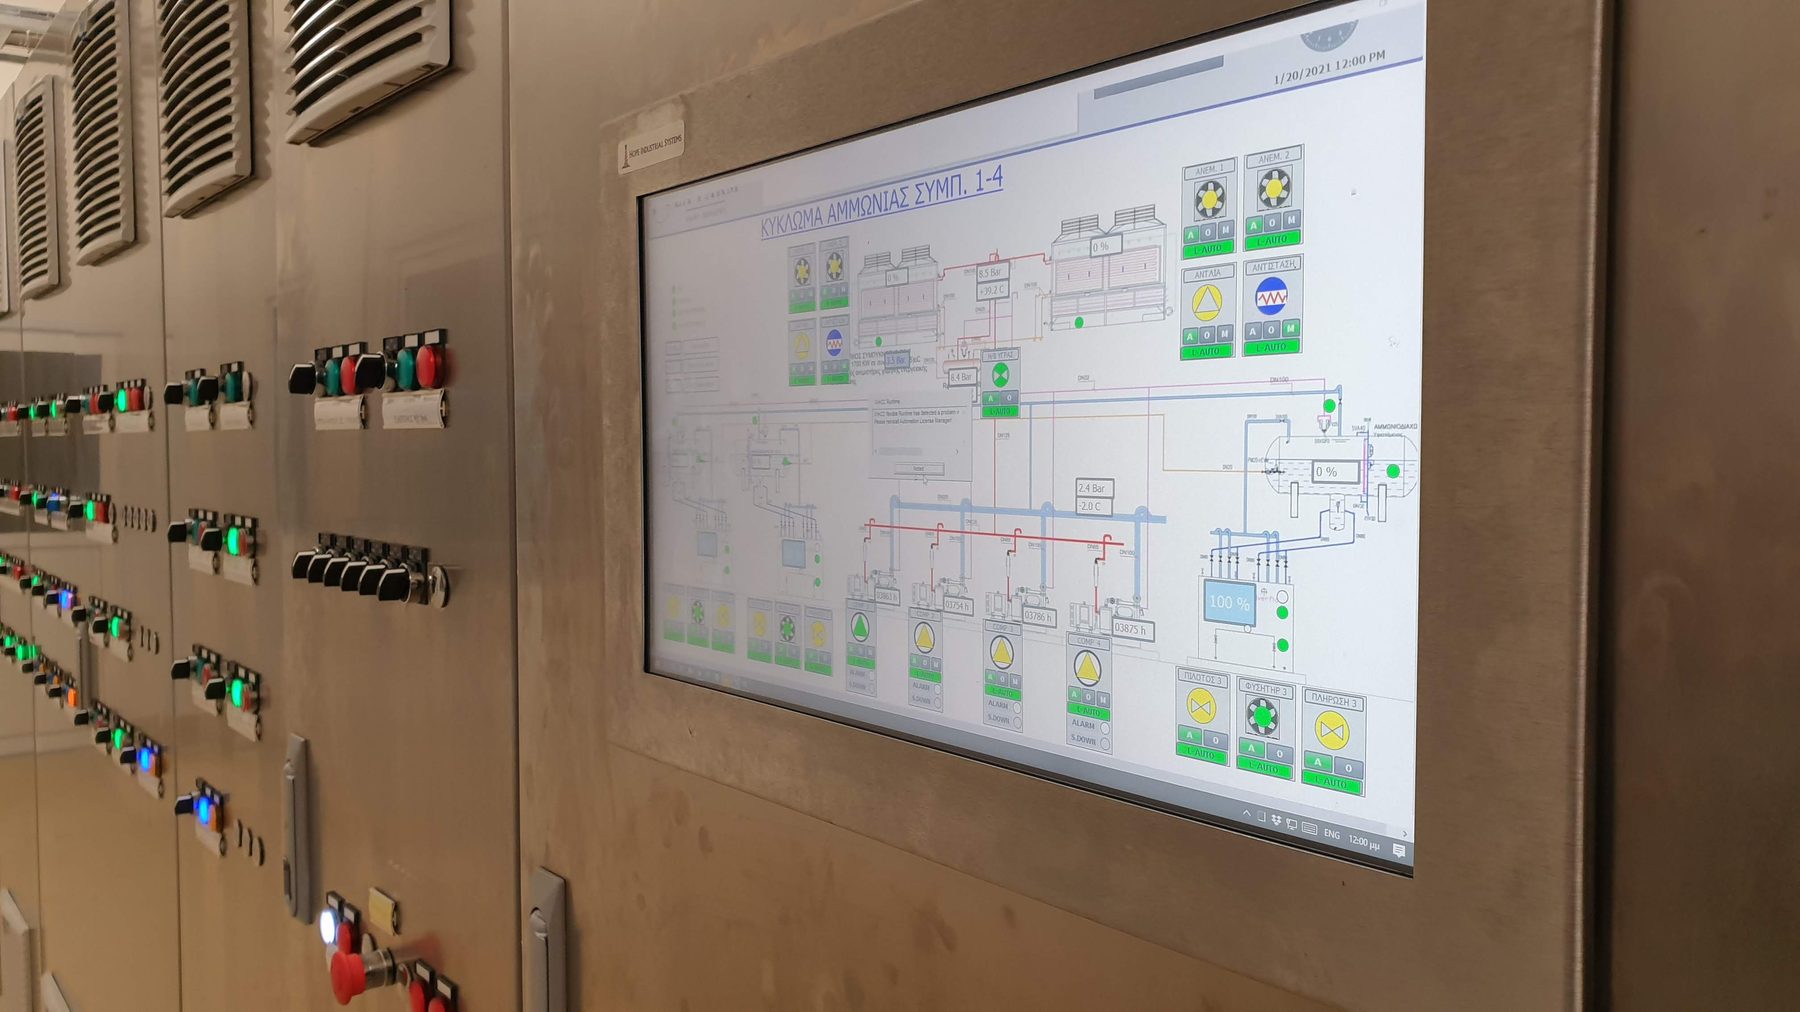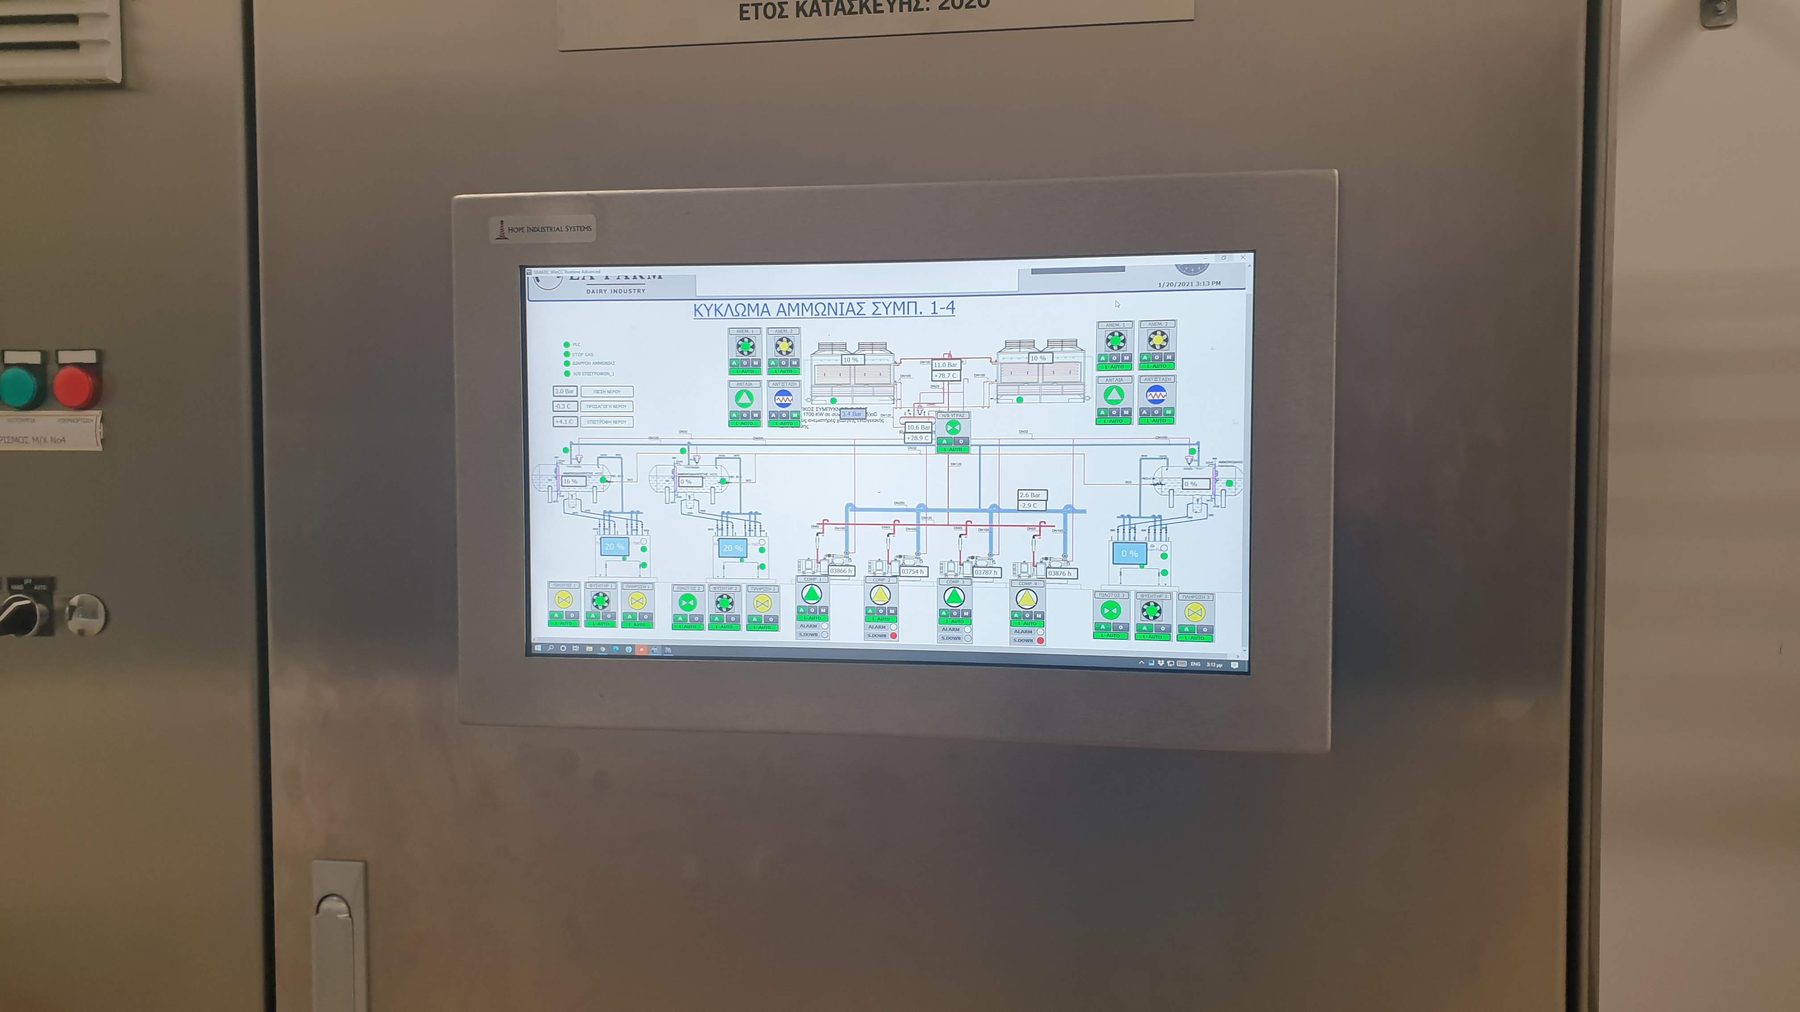
Control and supervisory automation for an ammonia machine room, with a central control panel and real-time SCADA monitoring.
KPautomation delivered the control automation for LA FARM's industrial refrigeration machine room, a multi-compressor ammonia installation critical to the plant's cold chain. The system monitors compressors, cooling towers and the ammonia circuit in real time through a central control panel and a supervisory control (SCADA/HMI) display, giving plant staff an immediate view of pressures, temperatures and the running status of every compressor.
Ammonia (NH3) remains one of the most energy-efficient refrigerants for large-scale industrial plants, but it is toxic and requires strict control of leaks, pressure and temperature. An ammonia machine room runs almost continuously around the clock, since any interruption to cooling can mean lost product or, in extreme cases, a safety risk to the plant and its staff. That is why the control automation has to combine continuous monitoring of pressure and temperature on every compressor, automatic safety interlocks that shut the plant down before it reaches dangerous limits, real-time alarm management, and redundant systems so that the failure of a single component doesn't halt the entire process.
A well-designed control system doesn't just protect the equipment — it protects the people, the product and the continuity of production. That's why the design, programming and testing of an ammonia automation system demand real experience and close attention to every detail.